Chemistry that makes industry cleaner.stronger.smarter.greener.
ALCO formulates and supplies high-performance water treatment, construction and specialty chemicals — engineered in Faisalabad, trusted by industry since 2015.
Leading the way in chemical excellence
Welcome to ALCO, where innovation, quality and sustainability converge to create industry-leading chemical solutions.
Established in 2015, ALCO has grown rapidly into one of Pakistan’s largest and most diversified chemical companies. Our journey from a humble trading company to a major producer and marketer of premium chemical products reflects our commitment to excellence and customer satisfaction.
New technologies, constantly explored.
The cornerstone, from R&D to service.
Responsible products and practices.
Six categories. One trusted partner.
Exceptional products for a wide range of industrial needs — each designed to enhance efficiency, performance and sustainability in your operations.
View the full range 01
Water Treatment Chemicals
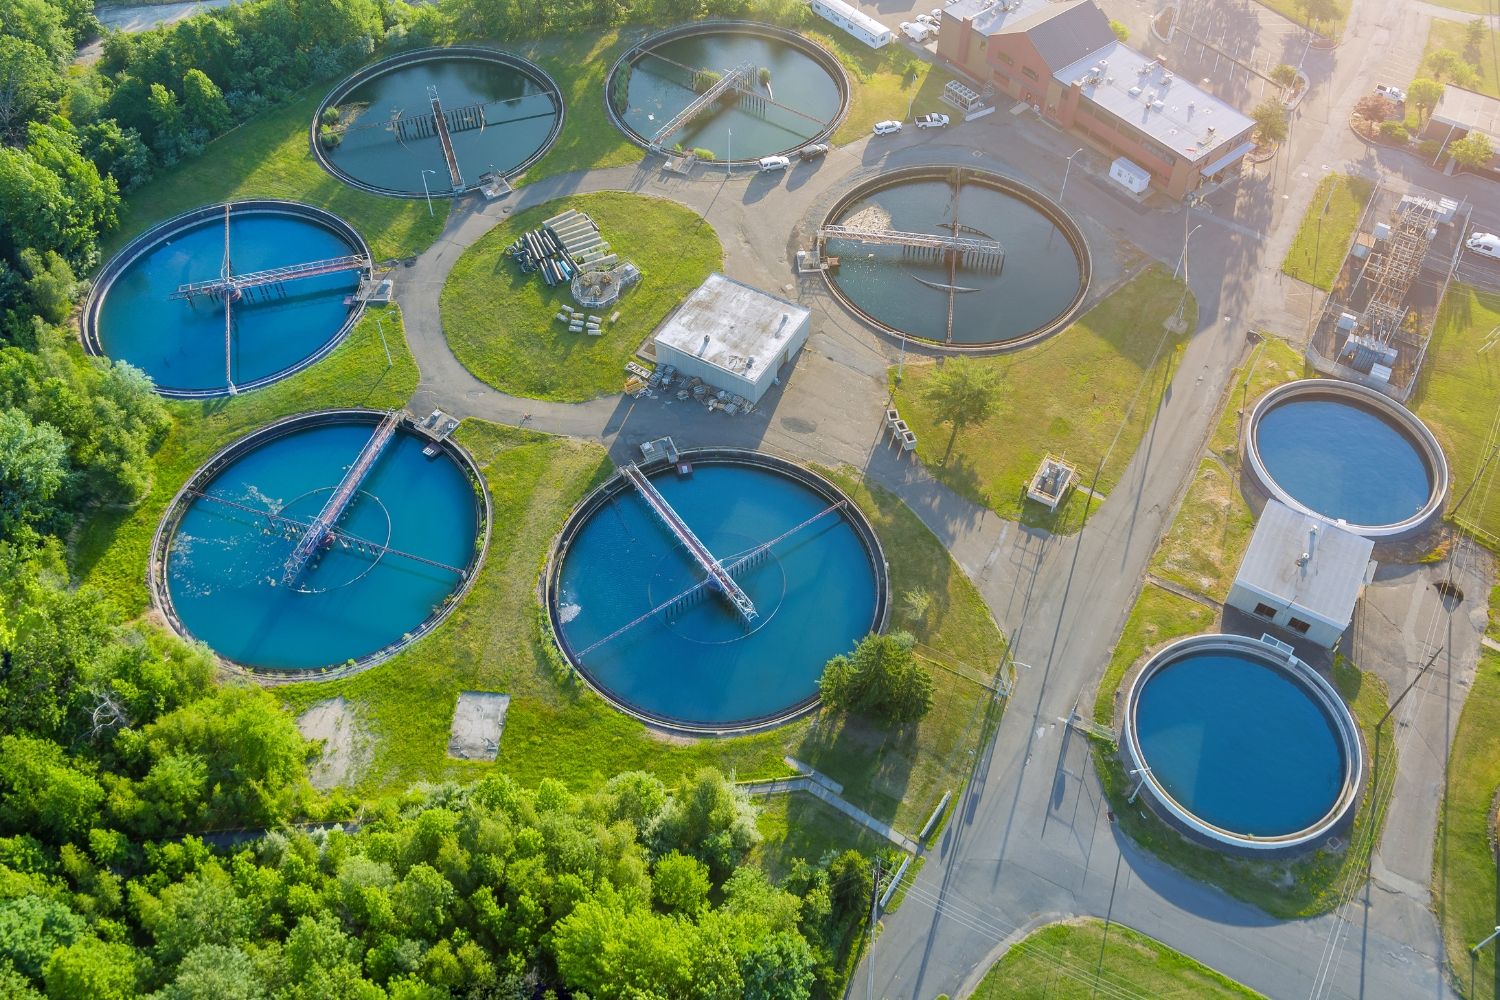
Comprehensive solutions for water treatment that enhance quality and efficiency across every application — clean, safe and reliable water management.
- Boiler Water Chemicals
- Cooling Water Chemicals
- Drinking Water Chemicals
 02
Construction Chemicals
Innovative solutions for the construction industry that enhance the strength, durability and performance of concrete structures.
- Ready-Mixed Concrete Admixture
- Precast Concrete Admixture
- Watertight Concrete Technology
 03
Teflon Coatings
High-performance PTFE coatings with exceptional non-stick, heat-resistant and chemical-resistant properties for industrial use.
 04
Antifoam & Defoamers
Effective defoaming solutions that control and reduce foam in industrial processes, ensuring smooth and efficient operations.
- Silicone Based Defoamer
- Non-Silicone Based Defoamer
 05
Pigment Dispersions
Advanced pigment dispersions that deliver consistent color, stability and ease of use across industrial applications.
 06
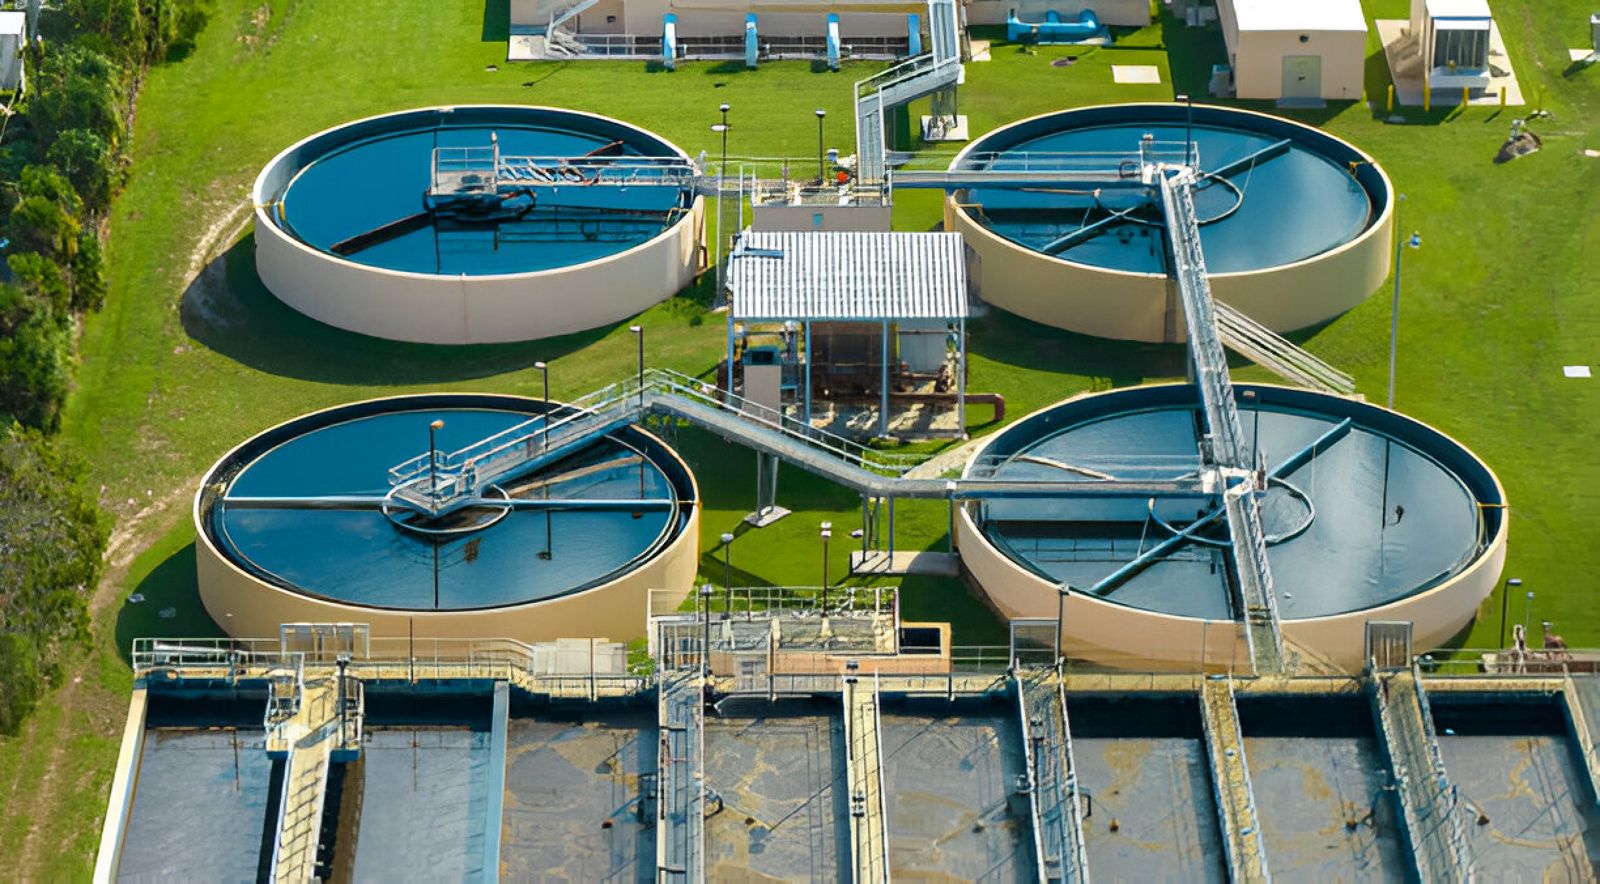
Effluent Chemicals
Specialised effluent treatment chemicals to manage and treat wastewater while ensuring compliance with environmental standards.
Solutions engineered for your sector
From power plants to paint lines, our chemistry keeps critical processes running.
01Water & Utilities
Municipal and industrial water purification, RO and drinking water.
Explore solutions 02
Construction & Infrastructure
Admixtures and watertight technology for bridges, towers and tunnels.
Explore solutions 03
Paints & Coatings
Pigment dispersions and defoamers for paints, inks and coatings.
Explore solutions 04
Power Generation
Boiler and cooling water programs that protect critical assets.
Explore solutions 05
Food & Beverage
Safe drinking water and process-compatible foam control.
Explore solutions 06
Pharmaceuticals
High-purity, non-contaminating process chemicals.
Explore solutions 07
Manufacturing
PTFE coatings and process aids that reduce downtime.
Explore solutions08Wastewater & Effluent
Compliance-ready effluent treatment for cleaner discharge.
Explore solutions
Chemistry for a
cleaner tomorrow.
Our range of drinking water, reverse osmosis and biomass water treatment solutions is designed to exceed industry standards while minimising environmental impact.
Lower dosages and longer equipment life mean less waste.
Responsible ingredients that support green building goals.
Effluent solutions that meet local and international standards.
Excellence in every step
Success is built on meticulous processes. Our systematic, customer-centric method delivers optimal results on every project.
Understanding Your Needs
We consult closely with you and assess your system to fully understand your requirements and goals.
Customized Development
Our R&D team formulates tailored solutions that deliver optimal performance and efficiency.
Rigorous Quality Assurance
Stringent testing ensures every product is effective, safe and reliable before it reaches you.
Ongoing Support
Continuous monitoring, technical assistance and optimisation keep your results at their best.
The ALCO advantage
Choosing the right chemical partner is crucial to your operations. Here’s why industry leaders choose ALCO.
Unmatched Quality
Strict quality control and assurance mean every product is reliable, effective and safe — consistent superior performance you can trust.
Innovative Solutions
Our R&D team continually explores new technologies, giving you access to the latest advances in process efficiency.
Comprehensive Support
Technical assistance, troubleshooting and ongoing optimisation — a reliable partner committed to your success.
Hear from our satisfied clients
Let’s solve your process challenge together
Tell us about your system, water analysis or project. Our specialists will recommend the right product and dosage — and reply within 24 hours.
- Site assessment & sampling
- Product & dosage recommendation
- Ongoing performance monitoring